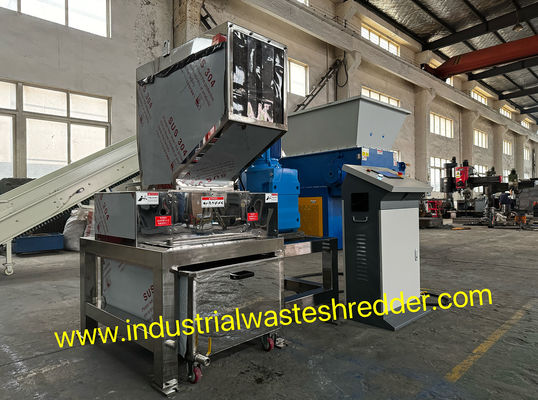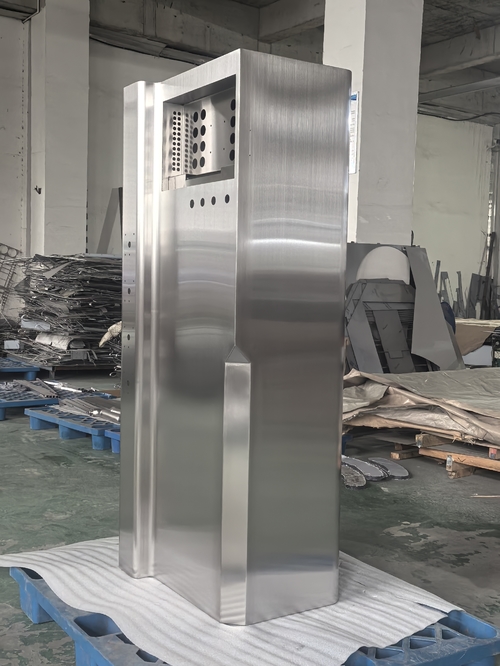
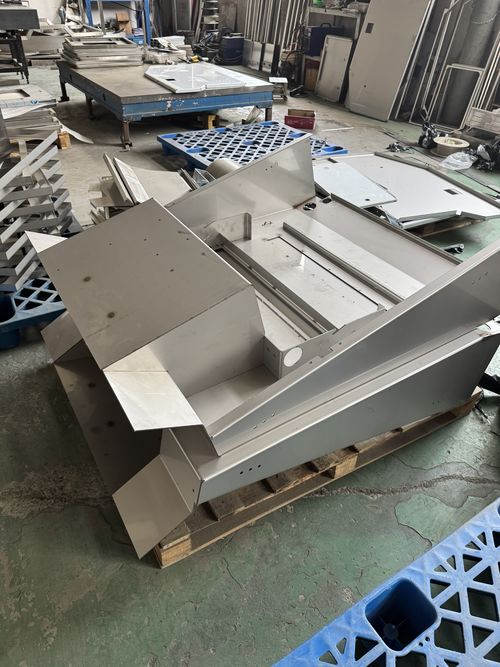
Project snapshot: a UK manufacturer of recycling and material sorting equipment needed a stainless steel fabrication partner for 316L hoppers, guards and control enclosures. Over 14 months the project moved from a single trial order to a quarterly release schedule, with lead time reduced by 35% and first-pass yield raised from 88% to 98.5%.
Client Background
ItemDetail
IndustryRecycling and material sorting equipment
LocationUnited Kingdom
Company sizeMid-sized OEM, 120 to 150 staff
Parts in scope316L hoppers, side guards, control cabinets, mounting frames
Annual volumeAround 2400 fabricated assemblies
Service usedOEM sheet metal fabrication, welding, powder coating, kitting
The Problem
The client had been buying fabricated 316L parts from a local UK subcontractor. Three issues kept repeating. First, delivery slipped: quoted at 8 weeks, actual delivery ran to 12 weeks in peak season, which pushed machine assembly dates and forced expensive overtime. Second, weld quality was inconsistent. Hoppers that must hold liquid were failing leak tests on roughly one unit in eight, and rework had to be done after powder coating, which meant stripping, re-welding and recoating. Third, dimensional drift appeared on multi-part assemblies: brackets that passed inspection individually would not line up on the assembly line, because each part had been made from a different drawing revision.
Cost per part looked acceptable on paper, but the true cost including rework, line stoppage and air freight for urgent replacement parts was far higher than the purchase price suggested.
What We Changed
Drawing and revision control: one master drawing set was locked at project start, and every batch was produced against the same revision with a revision stamp on each part
Welding fixtures: jigs were built for the three highest-volume weldments so hoop distortion stayed within 1.5mm and leak tests became repeatable
First article approval: a full first article with CMM dimensional report and weld photographs was approved before any batch production
Material traceability: 316L mill certificates were filed per heat number and referenced on the packing list
Kitting: parts for one machine were packed and labelled as a kit rather than as bulk quantities, cutting line-side sorting time
Surface treatment: powder coating applied after all welding and leak testing, with 480-hour salt spray verification on test coupons
Execution Timeline
Week 1: drawing review, DFM report issued with 11 cost and quality suggestions
Week 2: quotation approved, NDA signed, welding jigs designed
Week 3 to 4: first articles produced and shipped by air for approval
Week 5: client engineering sign-off, minor bend radius change incorporated
Week 6 onwards: batch production in 3-week cycles, sea freight with 2 weeks buffer stock at client site
Results After 14 Months
MetricBeforeAfter
Average lead time12 weeks7.5 weeks
First-pass yield88%98.5%
Leak test failures per batch12 unitsFewer than 1 unit
Rework and recoating costBaselineDown 42%
Emergency air freight events5 per year0 in 14 months
Assembly fit-up complaintsRecurringNone since batch 2
Client Feedback
"The difference is predictability. We stopped building buffer stock to protect our assembly line, because the parts arrive when promised and they fit the first time," said the client's purchasing manager. "The DFM notes in the first quote paid for themselves in the first three batches."
Why The Project Worked
Three things made the difference: fixtures instead of skill-dependent welding, one locked drawing revision across every batch, and inspection data shipped with the parts so the client could verify rather than guess, and a single English speaking engineer accountable for the account.
Similar Project?
We fabricate 304 and 316L parts for recycling equipment, food machinery, medical housings and water treatment systems. Send your drawing with material, thickness, finish and annual quantity, and our engineering team will reply with a costed quotation and DFM notes within 12 working hours.
حلولنا
✨ نحن نقدم خدمات تصنيع الصلب المقاوم للصدأ من نهاية إلى نهاية لمساعدة العملاء على حل التحديات في الدقة والجودة والتسليم.
✅ الحلول الرئيسية
تصنيع مخصصقطع معدنية من الفولاذ المقاوم للصدأ مصممة حسب الطلب بناءً على رسومات أو عيناتحسب الرسم أو العينة تخصيص قطع القطع من الفولاذ أو الذهب
التحكم بالجودة والدقةإدارة صارمة للتسامح وتفتيش 100% قبل الشحنإدارة الاختلافات الصارمة، فحص 100% قبل الشحن
إنتاج مرنمن النماذج الأولية إلى الطلبات الكبيرة، نتكيف مع احتياجاتك.من النموذج الصناعي، الطلبات الصغيرة إلى الطلبات الكبيرة متوافقة
وقت تسليم سريعالتصميم السريع للنماذج الأولية والإنتاج الفعال لتلبية الجداول الزمنية العاجلة.إنتاج سريع وفعال ومتوافق مع المدة الطارئة
خدمة واحدةدعم التصميم، قطع الليزر، الانحناء، اللحام، التشطيب السطحي، والتجميع.提供设计支持,激光切割,折??,接,表面处理到总装配的全过程服务.
بصفتنا شركة تصنيع محترفة لأعمال الصفائح المعدنية المصنوعة من الفولاذ المقاوم للصدأ، فإننا نقدم خدمات معالجة شاملة لتصنيع حاويات المعدات المخصصة. من المواد الخام للصفائح إلى المنتج النهائي المجمع بالكامل، يتم إكمال كل خطوة بدقة لتلبية معايير الجودة الدولية. فيما يلي سير العمل النموذجي لإنتاج حاويات معدات الفولاذ المقاوم للصدأ:
1. اختيار المواد والقطع
نبدأ باختيار صفائح الفولاذ المقاوم للصدأ عالية الجودة (مثل SS304 أو SS316). بناءً على رسومات العميل، تتم معالجة المواد باستخدام القطع بالليزر, القص باستخدام الحاسب الآلي, أو التثقيب لتحقيق أبعاد دقيقة وحواف نظيفة.
2. الثني والتشكيل
يتم تشكيل الأجزاء المقطوعة باستخدام مكابح الضغط CNC لضمان زوايا ثني دقيقة والتحكم في التفاوتات المتسقة. يمكن تحقيق الأشكال المعقدة من خلال عمليات الثني أو الدرفلة متعددة الخطوات.
3. التشغيل الآلي باستخدام الحاسب الآلي والمعالجة الثانوية
بالنسبة للمكونات التي تتطلب دقة أعلى أو ميزات خاصة، فإننا نقوم بـ الطحن باستخدام الحاسب الآلي, الاستغلال, التغويص, و الحفر لتلبية المتطلبات الوظيفية التفصيلية.
4. اللحام والتجميع
نستخدم لحام TIG, لحام MIG, اللحام البقعي, أو لحام المسامير لربط الأجزاء وفقًا للاحتياجات الهيكلية. بعد اللحام، يتم تجميع المكونات للتحقق من الملاءمة والاستقرار.
5. معالجة السطح
لتعزيز المظهر والمتانة، نقدم خيارات تشطيب متعددة، بما في ذلك:
الطحن والتلميع
التنظيف بالفرشاة
السفع الرملي
الخمول أو الطلاء المضاد لبصمات الأصابع
تعمل هذه المعالجات على تحسين مقاومة التآكل وتحقيق التأثير المرئي المطلوب.
6. فحص الجودة
يخضع كل جزء لفحص الأبعاد الصارم، وفحوصات جودة اللحام، والاختبارات الوظيفية. يضمن فريق الجودة لدينا أن جميع المكونات تلبي مواصفات العميل والمعايير الدولية قبل التعبئة.
7. التعبئة والشحن النهائي
يتم تنظيف الحاويات النهائية وحمايتها بغشاء/رغوة وتعبئتها بشكل آمن للتصدير لضمان التسليم الآمن للعملاء العالميين.